Heat treatment
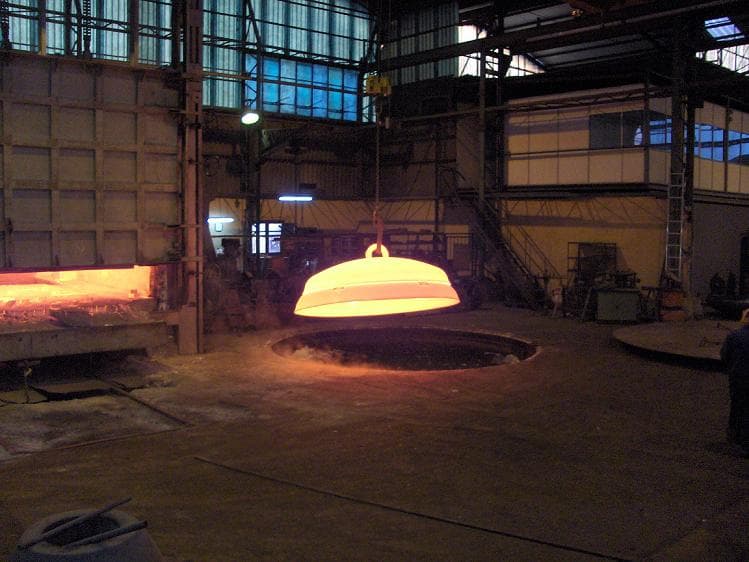
A gas furnace, measured and recorded.
The furnace reaches 1,200 °C. Calibrated thermocouples control it and the cycle is recorded. When needed, temperature is taken with thermocouples fixed to the part. The furnace has a quench bath.
Usual cycles
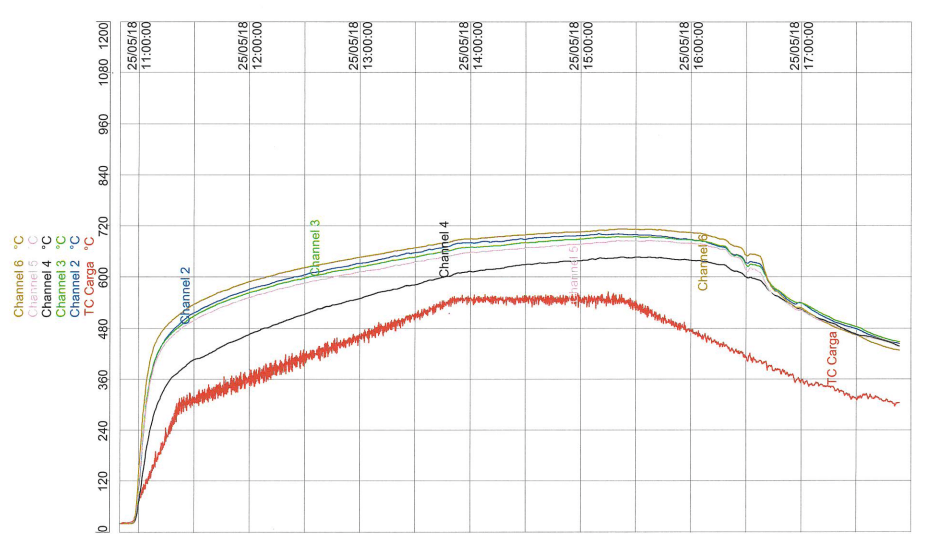
Stress relieving
600–620 °C.
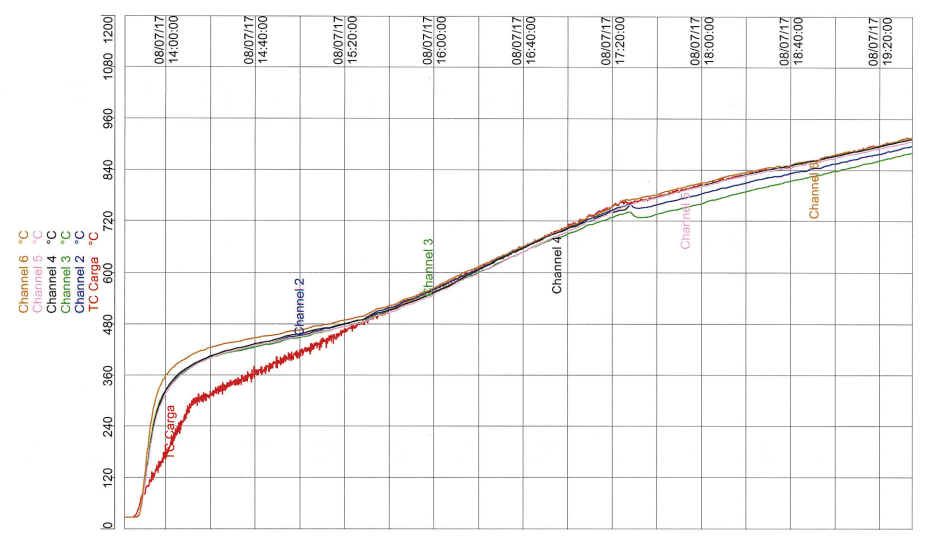
Normalising
920–950 °C, carbon steel.
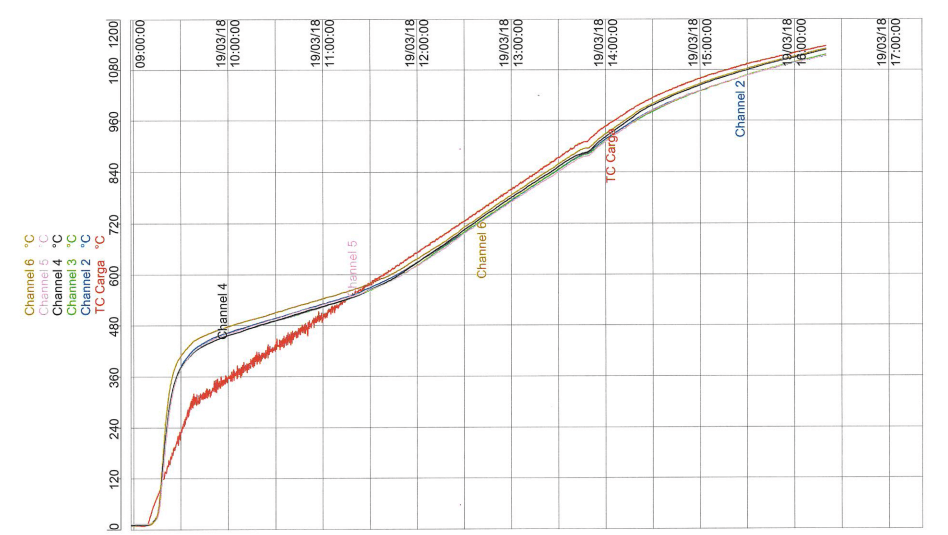
Solution annealing
1,050–1,100 °C for stainless, duplex, super duplex and nickel alloys, then a water quench.